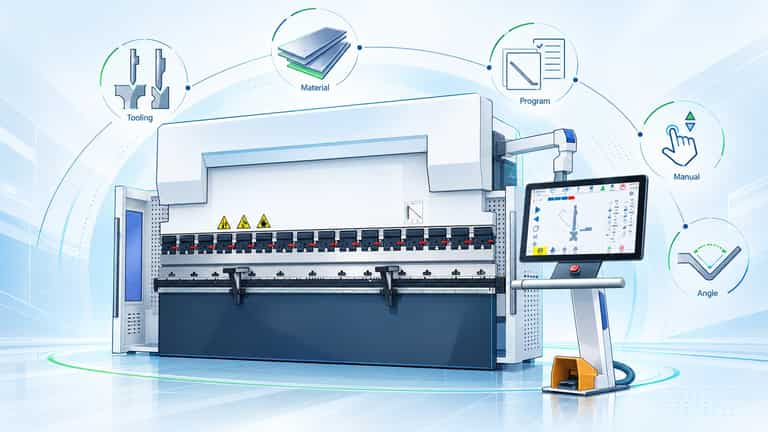
Choosing a China press brake is not only about comparing bending force, machine dimensions, or purchase price. International buyers also need to understand how the CNC controller fits their daily work: how quickly operators can prepare tooling, how material information is managed, how bending steps are programmed, and how the workshop verifies a finished angle. Those details influence training, changeovers, quality checks, and the practical value of a machine after installation.
This guide uses the KRRASS PA-15TX controller, primarily applied to the company’s StandardBend hydraulic CNC press brake range, to explain five real operating procedures. It combines an embedded video with precise interface instructions, fundamental bending knowledge, worked numerical examples, and a purchasing checklist for businesses evaluating a China-made CNC press brake. The goal is to help an operator complete the task on the screen while giving a production manager enough context to judge the complete bending system.
In the filmed demonstration, the operator enters tooling information, selects material data, creates a Product (the controller’s term for a bending program), uses Manual Mode, and corrects a measured 92° trial bend toward a specified 90° result. The measurement example belongs to that actual recorded job. It should not be interpreted as a guaranteed accuracy figure for all metals, tooling combinations, or machine configurations.
If you are comparing suppliers, you can also review the broader KRRASS press brake product range and KRRASS company and factory information. The sections below connect what happens on the PA-15TX screen with what matters on a production floor.
Watch the China Press Brake Controller Video: PA-15TX in Action
Open the complete PA-15TX video tutorial on YouTube if the player does not load in your browser.
| Time | Demonstration | Practical outcome |
|---|---|---|
| 00:06 | Add and edit punches and dies | Create, revise, and select tooling records |
| 01:30 | Select and add materials | Choose a library entry or define material properties |
| 01:44 | Create a Product in Automatic Mode | Set up and manage a multi-step bending program |
| 02:56 | Operate in Manual Mode | Prepare a straightforward single-step bend |
| 03:13 | Perform bending angle correction | Check a trial bend and enter a measured angle correction |
These chapter times correspond to the video, not to a generic training syllabus. For first-time operators, watch the five lessons in order. For experienced technicians, use the time markers to revisit a specific command before setting up the next job.
Why a China Press Brake Controller Tutorial Matters to Buyers
A CNC controller is an interface between the drawing, the operator, and the physical press brake. It stores instructions, but it cannot independently overcome an incorrect die, unsuitable bending tonnage, a damaged backgauge, inconsistent material, or unsafe setup. That is why the most useful test of a China press brake controller is not a menu screenshot; it is whether a trained operator can convert representative drawings into correctly measured parts using the actual machine and tools.
KRRASS manufactures sheet metal machinery in Nanjing, China, and offers multiple CNC press brake configurations. For the application covered by this tutorial, the relevant machine family is StandardBend, a hydraulic CNC press brake platform. The PA-15TX has a touchscreen workflow for recording punches and dies, handling the material library, creating Product programs, switching to manual operation, and applying angle correction. Those are the functions that this video actually demonstrates; capabilities beyond them should be confirmed against the quoted machine and software version.
For an overseas customer, three separate questions should guide the buying decision. First, does the machine have enough capacity and working length for the part family? Second, do the installed tool package and controlled axes support the required profiles? Third, can local operators learn, document, and repeat the workflow? A China press brake may offer a compelling purchasing proposition, but the answer depends on technical fit, commissioning, and total operating cost rather than nationality alone.
The PA-15TX and StandardBend Relationship
The PA-15TX controller is primarily used with the KRRASS StandardBend product line for the configuration discussed here. It should not be assumed to be the default controller for every StandardBend model: availability can vary by order, hardware package, and machine options. The StandardBend specification page presents machine capacities, working lengths, backgauge choices, tooling, safeguarding, and accessories. Ask KRRASS to identify the controller explicitly in your quotation and technical drawing set.
A well-matched machine specification also identifies ram stroke, daylight, throat depth, motor or hydraulic package, backgauge axes, safety protections, power requirements, tooling standard, and the factory acceptance test. These items matter as much as the touchscreen itself. The video demonstrates operator workflow; the final purchase agreement should define the performance and equipment being supplied.
Prepare the Machine and Job Before Programming
Before opening a menu, prepare the part drawing, material grade, verified sheet thickness, bending length, target angle, flange dimensions, inside-radius requirement, and desired bending sequence. Identify the punch and lower die that will physically be installed. Check whether the part will collide with the upper tooling, the ram, or a previously formed flange during later steps. Review the actual job before entering assumptions into the controller.
Inspect clamping, tool seating, the backgauge, the emergency stop, and the machine’s guarding according to the manufacturer’s procedures. Keep hands out of the point of operation, and use approved machine setup and isolation methods. The OSHA powered press-brake machine-guarding guidance describes serious point-of-operation hazards; it is a useful external reference, although the legal standards for a particular factory depend on its jurisdiction.
For a China press brake imported into another market, the buyer should also verify that guarding, manuals, electrical supply, and site arrangements meet the applicable local rules. A CNC program is never a substitute for appropriate safeguards or trained personnel. When equipment is delivered, retain the accepted part drawing, setup records, and inspection report so future operators can reproduce the initial demonstration.
PA-15TX Tutorial 1: Add and Edit Punches and Dies
Video begins at 00:06. Punch and die libraries are a practical foundation for CNC press brake programming. The punch shapes the inside of the bend and provides clearance for the part; the lower die supports the sheet and sets the opening. Recording the correct geometry lets operators retrieve a known setup instead of relying on memory or a handwritten note. A mismatched library entry can produce an incorrect starting calculation even when the physical tools are not damaged.
How to Add a Punch
- On the standby screen, tap the Punch icon along the upper edge of the display.
- When the Punch list appears, tap New on the right.
- In Add Punch, enter an easily recognized Punch Name and tap Confirm.
- Return to the list and select the relevant parameters if values need to be updated.
- For detailed changes, highlight the punch and tap Edit to open Edit Punch.
- Enter the dimensions indicated by the on-screen punch diagram; cross-check them against the installed tool and supplier drawings.
- Tap Confirm to save. To use another punch, reopen the punch list, select its name, and confirm the selection.
Tool names should be understandable to every shift. A useful internal naming convention might include tool shape, angle, nose radius, and segment length. For example, the company could assign consistent codes to straight punches and gooseneck punches and put matching identifiers on storage racks. The labels are your shop’s records, not a required PA-15TX format.
How to Add and Select a Die
- From the standby interface, tap Die at the top of the screen.
- Tap New and enter the new Die Name in Add Die.
- Tap Confirm to create the record.
- Highlight the die and tap Edit to adjust its geometry using the Edit Die diagram.
- Confirm the entry, then return to the Die list whenever you need to select another opening or die profile.
- Select the intended die name and tap Confirm to activate it for the job.
When a multi-V die is used, check its physical orientation and the active opening before starting. The actual V opening must match the library record. With the wrong opening, the operator may get an unexpected inside radius, minimum flange requirement, or bending force. This is why the KRRASS press brake tooling guide treats tooling selection as part of the complete process, not merely an accessory purchase.
V-Die Opening: A Simple Numerical Reference
For many conventional mild-steel air-bending jobs, using a lower-die opening around 6–10 times the sheet thickness is a preliminary shop-planning range. An 8× thickness opening is a convenient teaching example, not a machine preset or universal rule. Final selection depends on the material grade and strength, inside radius, flange dimensions, tool capacity, and surface requirements. The operator should check the tool supplier’s chart and the actual drawing before bending.
| Sheet thickness | Illustrative V opening at 8 × thickness | Job-specific item to verify |
|---|---|---|
| 1.0 mm | 8 mm | Tool alignment and surface marking |
| 1.5 mm | 12 mm | Short flange and bend radius |
| 2.0 mm | 16 mm | Material grade and tool load |
| 3.0 mm | 24 mm | Minimum flange and available force |
| 4.0 mm | 32 mm | Radius, tonnage, and bending length |
| 6.0 mm | 48 mm | High-load tool rating and part handling |
A wider opening often reduces bending force but increases the naturally formed inside radius and minimum flange. A narrower opening can make a shorter flange possible but raises force and the likelihood of marking. In a quotation for a China press brake, specify the actual material and desired parts so that the included punch-and-die package is chosen for the application rather than from a standard list alone.
PA-15TX Tutorial 2: Select and Add Materials
Video begins at 01:30. The controller’s material library lets the operator select an existing entry or create a new one. Material is not merely a label: different grades can require different forces and produce different levels of springback. Accurate material records reduce the chances that a familiar program is applied to an unfamiliar sheet without checking the mechanical properties.
From the standby screen, tap the material icon to open the material library. Choose a material name and tap Confirm to use it. To add a material, tap Add, enter the material name, then complete Tensile Strength Rm and Young’s Mod E as shown by the controller. Note that some PA-15TX screen labels use nonstandard English spelling; this article uses the correct technical words while the video shows the actual menu commands.
Tensile strength, Rm, is a measure of the stress a material can withstand in tension before fracture, typically expressed in MPa. Young’s modulus, E, describes elastic stiffness and is expressed in units such as GPa. They serve different purposes: tensile strength influences forming force, while elastic behavior contributes to springback. Use a material supplier’s test certificate or approved engineering data for the specific grade and delivery condition instead of copying generic values without verification.
Keep Material Records Specific Enough to Be Useful
A broad entry such as “steel” may hide meaningful differences between mild steel, stainless steel, and high-strength steel. Even within a nominal grade, batch-to-batch changes and actual thickness can affect the result. A practical workshop might maintain a verified material list with grade, thickness range, supplier information, and date of approval, while only entering fields that the controller actually supports. Additional batch information may remain on a separate setup sheet.
This connection between material data and press force is supported by SSAB’s press-brake force guidance, which identifies tensile strength, plate thickness, bend length, and die width among the important factors. A responsible China press brake supplier should therefore request your usual material grades as well as your maximum thickness when recommending machine capacity.
PA-15TX Tutorial 3: Create a Product in Automatic Mode
Video begins at 01:44. On the PA-15TX screen, Product refers to the bending job or program. Product programming is where the earlier decisions about tools and material become an ordered manufacturing process. The interface offers Data and 2D Graphic entry choices. This filmed lesson uses Data, which is a straightforward starting point for operators learning the system.
Create the New Product
- Tap the Product icon at the top of the standby interface.
- Select New Product on the right side of the screen.
- Enter the product or job Name using your workshop’s agreed naming convention.
- Select the Data input method for this demonstration; 2D Graphic is another available choice.
- Set the Angle correction method. The screen offers Absolute and Relative; we use Absolute in the video.
- Enter the required Plate Thick (sheet thickness) and Plate Length (programmed bending length).
- Choose the appropriate material from the material library.
- Select the correct Punch and Die records, check every entry, and tap Confirm to create the Product.
The on-screen field names are reproduced where needed so that a viewer can follow the video without guessing. The intended technical terms are sheet thickness, bending length, punch, die, and angle-correction method. Whether the final machine also supports other graphical or automatic features should be confirmed from the delivered version and configuration.
Add or Delete Bending Steps
To add a bending step, tap the step number at the upper-left corner of the Product screen. Select New Step in the pop-up menu; the new step is inserted after the selected step. To remove an unnecessary step, return to the same menu and choose Delete Step. The currently selected step is deleted. Then select each step in order and complete its corresponding bending parameters.
For a part with multiple flanges, this is more than data entry. An incorrect sequence can make a later bend physically inaccessible, cause the return flange to strike tooling, or make the sheet difficult to support. Confirm the order against the drawing and the machine’s actual clearance. Before releasing production, use a qualified setup process and inspect a first article. This is especially important when a China CNC press brake is newly installed and the operator is becoming familiar with its backgauge and tooling arrangement.
What to Record in a Repeatable Bending Program
| Setup item | Why it matters | How to confirm it |
|---|---|---|
| Product name and revision | Prevents the wrong program being reused | Compare with released drawing |
| Material grade and thickness | Influences force and springback | Confirm stock certificate and measurement |
| Punch geometry | Affects contact radius and clearance | Verify installed punch against library |
| Die opening and profile | Influences flange, radius, and force | Check physical die orientation |
| Bend angle and sequence | Controls final shape and collision risk | Review each step against the part |
| First-article result | Documents the proven setup | Record measured angle and dimensions |
A practical document-control habit is to label programs with a part number and revision, approve the first part against a drawing, and preserve the tooling list with the job record. Those practices make CNC programs more valuable because they reduce reliance on one experienced operator’s memory.
PA-15TX Tutorial 4: Operate in Manual Mode
Video begins at 02:56. From the standby screen, tap Manual at the bottom to enter Manual Mode. Enter the basic parameters required by the current job and, after completing the machine’s normal safety checks, use the approved operating controls to carry out a single-step bending cycle. Manual Mode is useful for simple bends, setup verification, controlled trials, and training under competent supervision.
“Manual” does not mean the machine is free of automatic motion or hazards. Depending on the machine configuration, a ram or backgauge may still move under powered control. Do not assume that touchscreen access overrides safety systems or allows hands near the tooling. Before operation, verify the tool position and clearances, check the programmed values, use required support devices for large sheets, and ensure that all personnel are clear of moving parts.
A Fast Pre-Bend Checklist
- Confirm that the correct Product or manual parameters are displayed.
- Check the actual sheet grade, thickness, and orientation against the job sheet.
- Verify the punch, V opening, clamping, and tool load rating.
- Check that the workpiece can move through the bend without collision.
- Confirm machine safeguarding, communication, and operator readiness.
- Bend a trial piece when required, then measure it before continuing with the batch.
On a China press brake with unfamiliar tooling, an extra minute of verification is usually more valuable than accelerating the first cycle. Manual Mode is best treated as a controlled manufacturing tool, not a shortcut around planning or inspection.
PA-15TX Tutorial 5: Perform Bending Angle Correction
Video begins at 03:13. The fifth demonstration addresses an everyday press brake problem: the measured angle after unloading does not equal the programmed angle. In the filmed example, the intended result is 90°, but the first measured bend is 92°. The controller was previously set to Absolute correction, so the operator enters the observed 92° in the Angle Correct field and performs another trial. That second part measures 90° in the video.
| Measurement in the filmed example | Value |
|---|---|
| Programmed target angle | 90° |
| Angle after the first test bend | 92° |
| Selected correction mode | Absolute |
| Value entered in Angle Correct | 92° |
| Second measured angle | 90° |
This is a documented two-degree observed deviation in one demonstration, not a universal rule saying every two-degree difference should be corrected by the same command or numerical setting. In Relative mode, the required entry may follow a different logic. Always confirm which correction method is active and refer to the supplied software instructions before saving revised production settings.
Why Springback Causes an Angle Difference
Sheet metal undergoes both elastic and plastic deformation during bending. After the tooling is released, some of the elastic strain recovers; this recovery is called springback. The amount depends on material strength, thickness, forming radius, die geometry, and the bending process. It is one reason that a 90° drawing requirement cannot always be met by simply programming a nominal 90° operation without inspection.
The material producer SSAB explains springback in press-brake bending and reports that it tends to increase with steel strength and with die-width-to-thickness ratio. Its published technical examples show differences between specific high-strength steel grades under defined conditions. These published figures should be read as material- and test-specific illustrations, not universal correction values for the PA-15TX or StandardBend.
Create a Reliable Angle-Correction Routine
Use the same calibrated angle measuring method, measure at a consistent location, allow any required handling or cooling time, and verify the tool and material inputs before changing the program. When the first result is wrong, consider the entire setup rather than immediately entering compensation. A poorly seated die, incorrect thickness, an unverified material grade, or machine deflection can all produce variation that cannot be solved reliably by a single correction value.
For production release, measure a first article and document both the programmed angle and the accepted result. If the part has several bends, inspect the assembled geometry as well as individual bends. Where a customer requires especially tight tolerances, agree on an inspection method and acceptance limits before purchase or batch production. An accurate China press brake operation depends on the machine, the verified program, the tooling, the material, and the inspection process acting together.
Technical Reference: What Determines Press Brake Force and Quality?
A controller is an important part of the bending system, but it does not create force independently. Required tonnage and finished-part quality vary with material, thickness, opening, bend length, tooling geometry, bending method, and the press brake’s structural response. This is crucial for buyers comparing China press brake specifications because two machines of similar advertised tonnage may have very different included tool packages, working lengths, or axis configurations.
SSAB’s press-force reference identifies the mechanical and geometric variables needed to estimate the load and recommends validation through trials. A simplified trend for similar air-bending jobs is that force increases with bending length and with approximately the square of thickness, and decreases as V opening grows, when other inputs are held constant. This relationship is useful for understanding trade-offs, not for approving a real bend without a machine-specific tonnage calculation.
Three Planning Calculations That Make the Data Useful
Example A: Die width. A 3 mm sheet with an 8× starting rule gives V = 3 × 8 = 24 mm. That is the planning result in the earlier table. It does not determine whether the required inside radius or flange is achievable; the engineering team must check these constraints.
Example B: Bend length. Under a comparable forming method and unchanged cross-section, doubling a bend from 500 mm to 1,000 mm approximately doubles the total bending force. Consequently, a machine’s tonnage rating must be evaluated against the maximum actual bend length. The tooling must also be rated for the resulting load per unit length.
Example C: Thickness. For a simplified comparison with identical material, die opening, and bend length, increasing thickness from 2 mm to 3 mm gives a thickness-squared ratio of (3 / 2)² = 2.25. This illustrates why thicker material can rapidly increase required load. The ratio is not valid if the die opening or other factors change between jobs. Real quotations should use the selected tooling and verified bending calculation.
| Variable | Effect on bending | Practical control |
|---|---|---|
| Tensile strength | Usually increases required forming force as strength rises | Use verified grade or test certificate |
| Actual thickness | Strong effect on force and bend behavior | Measure the stock actually received |
| Die opening | Changes load, radius, and minimum flange | Use approved tooling selection charts |
| Bend length | Longer bends require more total load | Check full job length and rated capacity |
| Tool wear and alignment | Can cause angle or profile variation | Inspect and maintain punch and die |
| Machine deflection | May change angle across a long bend | Review applicable crowning and calibration |
| Springback | Alters final angle after unloading | Measure a trial and apply proper correction |
| Operator data and revision | Errors can make good hardware produce bad parts | Approve and preserve setup documentation |
No single data table replaces a capacity chart, documented machine limits, or a controlled shop trial. The value of these examples is that they give an international buyer sensible questions to ask before committing to a China press brake purchase.
How the PA-15TX Workflow Supports Production Economics
The commercial benefit of CNC control is not limited to bending speed. Factories spend time reviewing drawings, choosing tools, locating material, programming, checking the first article, reworking errors, and documenting batches. A well-maintained punch-and-die library and clear Product names may reduce preparation effort and make training more consistent. The improvement depends on the original shop practices; the video itself does not establish a measured productivity percentage.
Consider a hypothetical shop performing 40 setups each week. If better tooling records and approved programs save five minutes per setup, the potential time released is 200 minutes per week, or 3 hours 20 minutes. Over 50 working weeks, that equals approximately 167 hours. The arithmetic is straightforward, but the scenario is an illustrative planning model, not a certified PA-15TX performance result. A buyer should estimate the real benefit using their own mix of repeat and custom orders.
Other savings may arise from preventing scrap, avoiding program mix-ups, and making first-article inspection more consistent. Those outcomes cannot be guaranteed by controller choice alone. In many workshops, the most valuable change is a standardized setup process supported by the controller, consistent training, properly maintained tools, and clear responsibility for revisions.
For a manufacturer considering a China press brake, ask the supplier to demonstrate the entire chain with one of your drawings: tool selection, material selection, Product programming, trial bend, measurement, correction, and accepted part. This verifies much more than a sales brochure’s feature list and provides a meaningful basis for discussing operator training.
How to Choose a China Press Brake for Your Workshop
The term China press brake describes the origin of the machinery being considered, not a unique technical specification. Good purchasing decisions start with the required parts, followed by a review of machine capability and supplier support. KRRASS offers hydraulic CNC press brakes and other bending solutions, but the relevant product line for the PA-15TX workflow shown here is StandardBend.
Begin with material grades, maximum and typical thickness, bend lengths, short-flange needs, expected annual volume, and the tightest drawing tolerances. Then discuss frame and ram capacity, controlled axes, backgauge travel and fingers, crowning, tool clamping, guarding, electrical compatibility, and training. If the parts include boxes or return flanges, supply the drawings early so that tooling access and collision risks can be reviewed.
Published StandardBend Examples: Capacity Is Not the Whole Specification
The KRRASS StandardBend technical-data page lists machine sizes across multiple capacities. The following are examples of published model entries, not a promise that each is supplied with PA-15TX or that all options are identical.
| Published StandardBend example | Listed nominal force | Listed bending length | How a buyer should use it |
|---|---|---|---|
| PBS 50T/1600 | 500 kN | 1,600 mm | Evaluate smaller or shorter parts and available tooling |
| PBS 80T/2500 | 800 kN | 2,500 mm | Check medium-length work and typical grade/thickness mix |
| PBS 110T/3200 | 1,100 kN | 3,200 mm | Verify force for full-width parts and required axes |
| PBS 175T/4000 | 1,750 kN | 4,000 mm | Review long bends, handling, and deflection compensation |
These listed capacities are starting points for specification review, not application approval. An advertised bending length does not mean that the maximum machine force is suitable for every thickness and grade across that entire length. Demand a calculated load check for representative parts. The exact controller, backgauge, tooling, guarding, and other options must be identified on the final quotation.
Evaluate More Than the Quoted Machine Price
A low initial invoice can be offset by expensive tools, difficult changeovers, spare-parts delays, unsuitable site power, poor documentation, or slow commissioning. Conversely, an appropriately equipped China CNC press brake can be cost-effective if its capacity and service arrangements genuinely match the work. Compare machines using an agreed scope rather than treating two headline prices as equivalent.
Useful purchasing criteria include verified frame and hydraulic specifications, acceptance-test procedures, the manufacturer’s technical support route, replacement tooling compatibility, training, the software language and version, electrical documentation, shipping terms, and warranty scope. Ask for evidence relevant to your market. Avoid assuming that a supplier’s general certification claims automatically establish compliance for a particular machine at your installation site.
The Questions to Send a China Press Brake Manufacturer
A focused request for quotation helps the supplier propose a suitable machine and reduces the risk of an incomplete offer.
- Material: Which grades, thicknesses, and surface finishes will the machine process?
- Parts: What are the longest bends, shortest flanges, required inside radii, and tightest tolerances?
- Output: How many different setups and parts are expected per shift?
- Controls: Is the PA-15TX available on the specific StandardBend model being quoted, and what firmware and axes are included?
- Tooling: Which punches, V dies, adapters, and clamping systems are included, and what are their ratings?
- Safety: Which guards, laser systems, foot controls, and emergency-stop arrangements are supplied?
- Inspection: Can the supplier demonstrate a customer drawing and provide measurements for an accepted first article?
- Delivery: What site utilities, installation work, documentation, training, warranty, and spare-parts support are included?
If your business plans to buy a China press brake for mixed sheet metal production, send several typical drawings rather than only the most extreme one. A collection of representative parts reveals tooling, backgauge, and workflow requirements that a single maximum-capacity figure may conceal.

Frequently Asked Questions About China Press Brakes and PA-15TX
What is a China press brake controller?
A China press brake controller is simply the CNC or NC control unit fitted to a press brake manufactured or supplied from China. There is no universal controller specification defined by this phrase. A controller may provide tooling libraries, material data, backgauge programming, bend sequencing, and compensation functions depending on the model and machine. This article demonstrates the actual PA-15TX workflows visible in the KRRASS video.
Is the PA-15TX controller mainly used on KRRASS StandardBend?
Yes. For this KRRASS article, the PA-15TX is positioned primarily with the StandardBend hydraulic CNC press brake product line. Controller availability depends on the specific quoted machine configuration; confirm it in writing instead of assuming every machine includes the same system.
How do I add a punch or die on the PA-15TX?
Open Punch or Die, choose New, name the tooling record, and tap Confirm. Select Edit to enter or correct geometric parameters based on the actual tool. Choose the intended record and confirm before starting production.
Can the PA-15TX create a multi-step bending program?
The demonstrated Product screen supports adding and deleting steps. Tap the step number, select New Step to add a step after the current one, or Delete Step to remove the selected step. Set and verify the parameters for each stage, including the sequence and clearance.
What is the difference between Data and 2D Graphic?
They are two input options shown during New Product creation. The filmed operation uses Data programming. It does not demonstrate every available 2D Graphic command, so specific advanced functionality should be checked on the actual controller and software version.
What material properties are entered in the video?
The material workflow includes a name, Tensile Strength Rm, and Young’s Mod E. Use reliable values for the supplied material grade and condition; they are not interchangeable properties. Keep any supporting material certificate with the job documentation.
What does Absolute angle correction mean in the PA-15TX video?
In this particular demonstration, the target is 90° and the first measured result is 92°. With Absolute correction selected, the operator enters 92° into Angle Correct, then measures 90° on the second trial. Follow your controller’s correction-mode instructions; another setup can behave differently.
Does using PA-15TX guarantee a perfect 90-degree bend?
No. Final angle depends on material properties, thickness, tooling, machine condition, bending process, and measurement. The example establishes the recorded result of one job; it is not a universal performance guarantee. Always inspect the first part and confirm drawing tolerances.
What should I check when comparing China press brake manufacturers?
Compare actual parts and bending calculations, technical configuration, included tooling, safety equipment, factory test evidence, documentation, after-sales support, and the total delivered scope. A capable manufacturer should discuss your representative drawings and the process rather than relying only on a broad price or tonnage claim.
Where can I request a KRRASS StandardBend quotation?
Review the KRRASS StandardBend range, then use the official KRRASS inquiry form to send material grades, maximum bending lengths, part drawings, desired controller, and production requirements. Ask the team to confirm PA-15TX availability on the quoted StandardBend configuration.
Final Thoughts: From a Controller Tutorial to a Confident Buying Decision
The five PA-15TX demonstrations show the everyday sequence behind a repeatable CNC bend: tooling records, material selection, Product programming, manual operation, and measured angle correction. Together they give operators a practical starting point and provide production managers with concrete questions to ask about training, quality control, and workflow reliability.
For international customers searching for a China press brake, the lesson is broader than one controller. A useful investment combines a correctly sized machine, verified material and tooling data, safe operation, a repeatable programming process, and supplier support. Evaluate the complete system against representative parts rather than assuming that a model name or a low price ensures the required result.
Explore KRRASS StandardBend hydraulic CNC press brakes for the relevant machine family, compare the wider KRRASS press brake range, or contact KRRASS for a technical quotation with your drawings, material requirements, bending lengths, and preferred controller. You can also reach the team at [email protected] or +86 189 5208 7956, as listed on the official contact page.
Share